
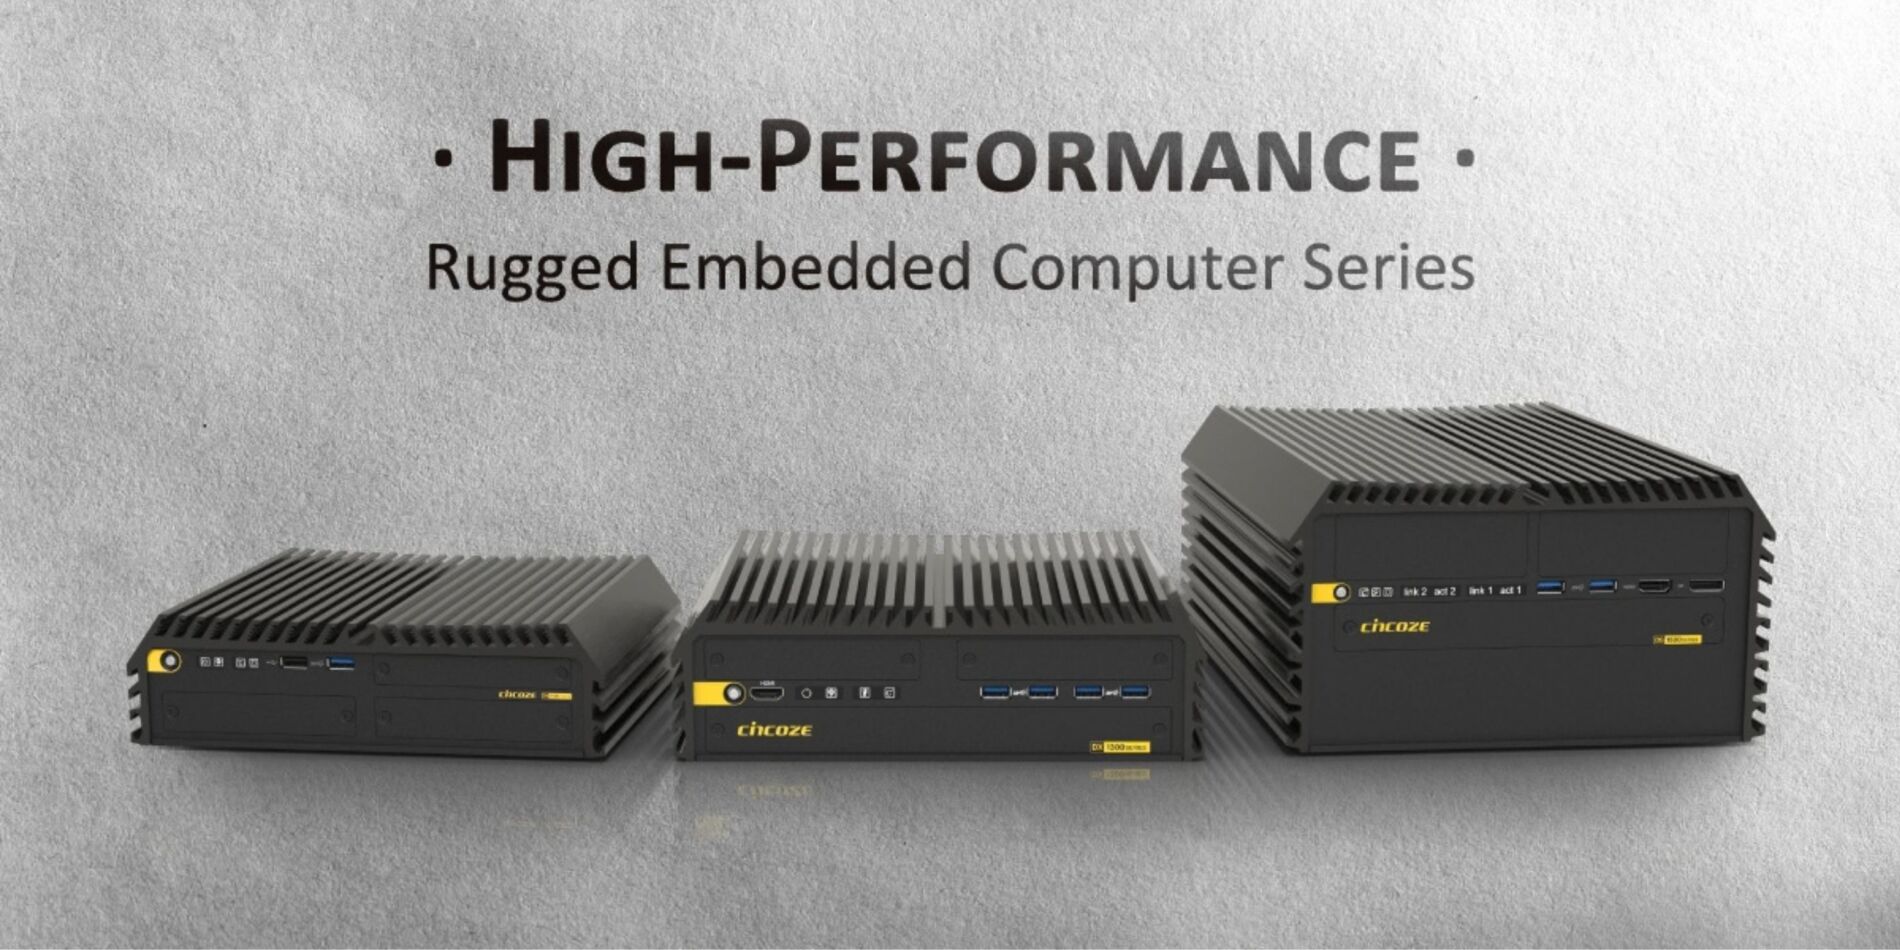
In modern industrial automation, machine vision, smart transportation, and Edge AI applications, deploying commercial off-the-shelf PCs in harsh environments is an unacceptable operational risk. Constant vibration, dust, extreme temperatures, and power fluctuations quickly degrade standard hardware, leading to unbudgeted downtime and costly repairs.
Cincoze high-performance rugged industrial computers are purpose-built to eliminate these failure points. Combining military-grade durability, modular expansion capabilities, and a maintenance-friendly mechanical design, Cincoze has become the trusted choice for critical industrial deployments.
Here is a breakdown of the three core pillars that make Cincoze the ideal solution for demanding industrial projects.
1. Diverse Certifications for Vertical Market Applications
Engineered from the ground up for extreme field conditions, Cincoze embedded computers deliver uncompromised operational stability against power anomalies and harsh climates:
-
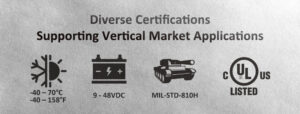
Extended Industrial Temperature Range: Supports continuous 24/7 operation in extreme temperatures ranging from -40°C to 70°C, making them ideal for outdoor enclosures, steel mills, and cold storage facilities.
-
Wide-Range Power Input: Accepts 9–48 VDC input voltages, protecting internal electronics against voltage spikes and brownouts common in industrial grids and vehicle power systems.
-
Military-Grade Shock and Vibration Resistance: Fully UL safety-certified, complying with international EMC standards (CE, FCC, UKCA), and tested to MIL-STD-810H military standards for shock and vibration endurance.
-
Specialized Vertical Industry Certifications:
-
Rail Transportation: Certified to EN 50121-3-2 (EMC) and EN 45545-2 (fire protection) for rolling stock and wayside signaling setups.
-
Automotive & Fleet Management: Features E-mark certification for seamless integration into heavy machinery, public transit, and logistics fleets.
-
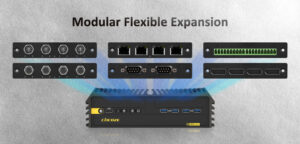
2. Modular Flexible Expansion (CMI & CFM Technology)
A major challenge when selecting an industrial PC is anticipating future I/O requirements without overspending on the initial build. Cincoze solves this through its proprietary CMI (Combined Multiple I/O) and CFM (Control Function Module) modular architecture:
-
Tailored Configuration: Select the exact I/O interface combination needed for your current application at the time of purchase.
-
Seamless Field Upgrades: Easily add extra COM, DIO, or LAN ports, or install functional modules such as PoE (Power over Ethernet for machine vision cameras), TPM (cryptographic security), and IGN (smart ignition sensing for controlled in-vehicle power management).
-
Lower Total Cost of Ownership (TCO): Avoid replacing the entire computer chassis when expanding production lines or adding new sensors.
3. Quick Operation and Easy Field Maintenance
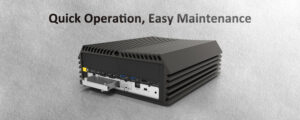
Minimizing Mean Time to Repair (MTTR) is critical in high-throughput plants and remote installations. Cincoze’s user-centric mechanical layout features a front-access maintenance design engineered for field technicians:
-
Chassis-Free Adjustments: The front maintenance area consolidates essential controls in one place—including the SIM card slot, CMOS battery, and key system configuration DIP switches—allowing technicians to make quick adjustments without disassembling the chassis.
-
Front-Access Drive Bays: Storage devices can be rapidly swapped or removed for routine maintenance or emergency data preservation during critical field events.
Technical Feature Overview
| Feature / Metric | Industrial Specification / Capability |
| Operating Temperature | Extended range from -40°C to 70°C |
| Input Voltage | Wide 9–48 VDC input with built-in power protection |
| Durability Testing | MIL-STD-810H military shock and vibration certification |
| Vertical Certifications | EN 50121-3-2 / EN 45545-2 (Rail), E-mark (In-Vehicle), UL, CE, FCC, UKCA |
| Modular Expansion | Proprietary CMI & CFM modules for COM, DIO, LAN, PoE, TPM, & IGN |
| Maintenance Design | Front-access panel for storage drives, SIM slots, CMOS battery, and switches |
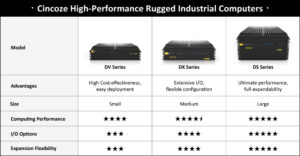
Partner with Logicbus for Cincoze Industrial Computing
At Logicbus, we are an official distributor and integration partner for Cincoze high-performance rugged industrial computers. Our application engineering team supports your project from hardware selection and modular configuration to system testing and deployment across North America.
-
Need a customized industrial PC for a high-vibration or wide-temperature environment?
-
Consult with our technical sales engineers to configure the optimal Cincoze setup for your application.
Contact Logicbus Today to Get a Quote & Custom Configuration
sales@logicbus.com | support@logicbus.com | +1 619 616 7350 | Start conversation